 CN Sweaters
A full-zip sweater should be approved as a system: the knit body, zipper, placket stabilization, care path, and final measurements must agree on the same dated sample record. A zipper is comparatively rigid beside a flexible knit, so the buyer needs evidence of how the assembled garment behaves before bulk release.
Lock the zipper type and length, placket construction, yarn and gauge, measurement points, intended care cycle, and acceptance plan before sampling. Ask the supplier to identify the proposed input, the approved reference, and the change-control step for each. This guide explains the verification path; it does not claim universal zipper sizes, shrinkage figures, MOQ, lead time, or factory test results. The supplier file should let a technical buyer identify the exact sample, inputs, care cycle, result, acceptance rule, and owner before any production release. If any one record is absent, the buyer should hold the next gate and request a dated correction rather than approve on assumption.
Which placket conditions must be approved?
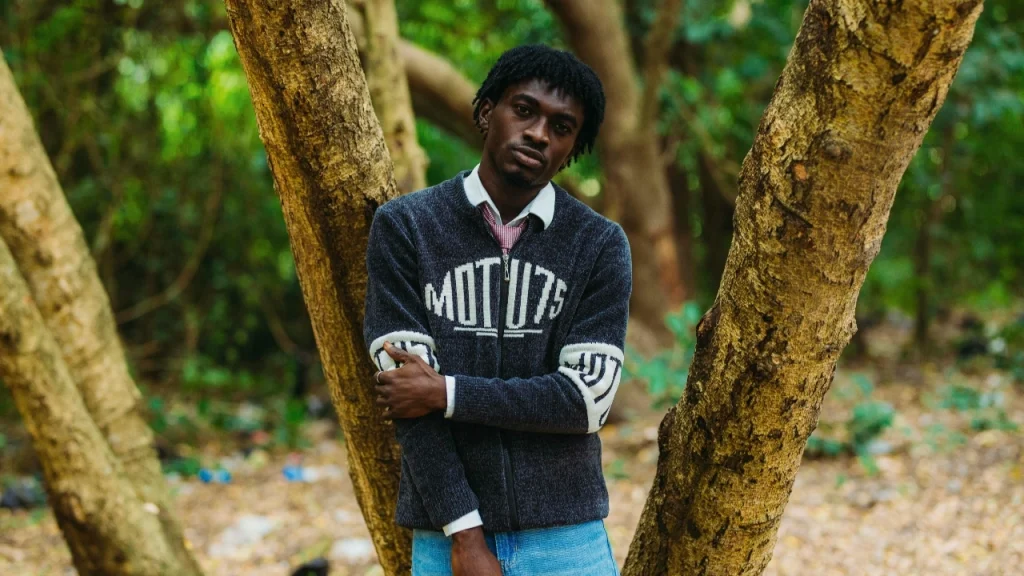
Placket buckling occurs when the zipper tape is sewn under excessive tension relative to the highly elastic knitted panels, causing the fabric to gather and wave. This physical mismatch escalates during washing as the knit panels shrink while the synthetic zipper tape remains dimensionally static.
Which assembly conditions can create waviness?
During sewing, the feed dog of a lockstitch or overlock machine naturally pulls the lower layer of fabric faster than the upper layer unless a specialized walking foot is utilized. When attaching a zipper to a full zip cardigan, any slight stretching of the knitted placket relative to the zipper tape causes immediate buckling once the garment is relaxed. To mitigate this on our factory floor, we utilize specialized sewing attachments that feed the zipper tape and the knitted panel at a strictly synchronized 1:1 ratio. This structural stability is essential for high-end knitwear like a custom full zip knit sweater to ensure the front closure remains completely flat.
Which stabilization detail belongs in the sample record?
The choice of edge stitching along the placket significantly affects the structural resistance against torquing. Utilizing knit structures that resist elongation, such as compact Milano ribs or full cardigan stitches, provides a stable platform for zipper insertion. According to the technical guidelines on CottonWorks Knit Basics, the configuration of courses and wales determines fabric behavior; without a dense, stable knit border, the tension from a zipper will warp the surrounding single-jersey loops. We often recommend integrating a fusible knit interfacing tape inside the placket fold to block the vertical stretch before the sewing needle pierces the fabric.
Which zipper specification fits the approved sample?
Selecting the correct zipper gauge requires matching the physical weight and tape width of the zipper with the specific machine gauge of the sweater to avoid structural collapse or fabric sagging. An excessively heavy zipper will drag a lightweight knit downward, whereas a flimsy zipper will fail to close smoothly on a heavy-gauge fabric.
Which zipper details must be compared against the knit?
Heavyweight knits, such as a 3GG or 5GG full zip cardigan sweater, demand robust closures like a #5 or #8 metal zipper to balance the physical presence of the thick yarns. Conversely, a fine-gauge 12GG or 14GG sweater full zip silhouette requires a delicate #3 nylon coil or lightweight molded plastic zipper to maintain its fluid drape. To assist sourcing managers in selecting the ideal combinations, we have compiled a standard manufacturing compatibility matrix that pairs sweater gauges with optimized zipper specifications.
Buyer input
Zipper type, length, tape colour, puller, yarn, gauge, care cycle and POM.
Evidence to request
Swatch or sample, approved placket detail, before-and-after measurements and change log.
Release decision
Approve only when the exact sample, input versions and acceptance plan agree.
This matrix demonstrates that lighter knit gauges require highly flexible, low-profile nylon zippers to prevent severe placket sagging, while heavier cardigans necessitate structurally reinforced metal zippers to sustain the weight of thick wool or cotton yarns.
Which care-cycle evidence protects the placket?
Different materials can respond differently to the specified care cycle. Rather than assume a generic shrinkage value, state the care method, specimen, measurement points, conditioning, accepted change, and decision owner. If the result changes the placket appearance or target fit, keep the sample on hold until the construction or care instruction is resolved.
Which knit structure keeps the panel balance?
The physical gauge of the knitting machinery defines the spacing of the needles, which directly governs the density, stitch length, and overall stability of the full zip sweater panels. Choosing a gauge without calibrating yarn ply and tension leads to loose, unstable structures that are highly prone to front panel distortion.
Which panel construction needs a documented control?
Circular knitting machinery excels at producing high-volume, continuous fabric tubes that are excellent for casual wear like active hoodies, but they require cutting and sewing which can introduce spirality. For a premium sweater, we utilize flatbed flat-knitting machines that knit panels to shape, allowing for precise control over the tension of every single course. This fully-fashioned knitting method eliminates cut-and-sew waste while ensuring that the left and right front panels have an identical stitch count, which is critical for zipper alignment. Many premium Sweaters rely on these flatbed mechanics to achieve uniform panel length.
How should stitch detail be checked for balance?
Different stitch combinations behave differently under physical stress. A standard knit stitch creates a classic jersey face, but adding tuck or float stitches changes the physical dynamics of the panel. As explained in the CottonWorks knitting resources, tuck stitches increase fabric width and thickness while reducing vertical extensibility, which can help stabilize the areas surrounding a zipper. Conversely, float stitches narrow the fabric and make it more rigid. If a designer incorporates asymmetric stitch patterns without balancing the tension, the entire front panel will torque, pulling the zipper placket to one side and ruining the garment’s fit. This torquing represents a major risk during bulk production if the yarn dye lots have slight variation in moisture absorption or elasticity. Our factory floor operators run continuous calibration checks on tension sensors to guarantee that every panel we knit remains within a strict 1% variance, ensuring a completely flat profile.
Which material and care variables need a wash decision?
Wool fibers possess microscopic surface scales that interlock when exposed to moisture, heat, and mechanical agitation, leading to felting shrinkage and severe placket distortion if the raw materials are not treated or washed correctly. This natural fiber movement creates a massive dimensional difference between the wool body and the synthetic zipper tape.
How should wool care be linked to the approved sample?
A premium full zip wool sweater offers exceptional breathability and comfort, but it is highly sensitive to laundering. When a customer machine-washes a wool garment, the fiber agitation causes the front panels to contract. Because polyester zipper tapes are chemically stable and unaffected by mild heat, the shrinking wool pulls the zipper into tight, unsightly waves. To combat this, we advise brands to specify machine-washable wool yarns that have undergone Hercosett shrink-resist treatments, which smooth the fiber scales. Utilizing established care protocols like those detailed in the Woolmark Wool Care guidelines ensures that the delicate wool fibers retain their shape and structural integrity over dozens of wash cycles.
Which before-and-after records support release?
To guarantee bulk production stability, our factory conducts relaxation washing on all pre-production samples. We measure the panels before and after laundering to calculate the exact residual shrinkage. If a knit fabric has a 4% vertical shrinkage, we program our flatbed knitting machines to knit the panels 4% longer than the target tech pack measurements. This ensures that after the first wash, the garment shrinks precisely to the desired fit without putting stress on the zipper tape. Without this careful calibration, the finished product will inevitably fail retail inspections. By pre-washing our sample swatches and correlating the data with our digital knitting files, we eliminate the guesswork from the initial prototyping stage.
Which pattern records protect left-right balance?
Perfect symmetry between the left and right front panels is the foundation of a balanced full zip cardigan. Even a minor variation of two millimeters in length or stitch count between the two front panels will result in a twisted zipper, misaligned necklines, and uneven hems.
Which paired-panel checks should be retained?
During flatbed knitting, environmental factors like temperature or yarn wax levels can cause subtle variations in yarn tension. If the left panel is knit under slightly higher tension than the right, it will be shorter and denser. When we sew the zipper onto these panels, the unequal tension forces the shorter side to stretch, causing the finished garment to pull to one side. We implement strict weight-per-panel quality checks on the factory floor, weighing each left and right panel on digital scales before assembly to ensure they are identical to within a fraction of a gram.
Which construction details need an approval point?
The lower hem of a full zip knit sweater is another common failure point. Standard 1×1 or 2×2 ribbing on the hem must be knitted with elastomeric spandex yarn fed into the structure to prevent the hem from blowing out or stretching permanently. Furthermore, shoulder seams must be reinforced with clear polyurethane tape or twill tape during the joining process. Without this reinforcement, the weight of the sleeves and the front zipper will pull the shoulder seams downward, causing shoulder seam unevenness and distorting the chest fit of the garment. For high-performance outerwear like Zip-Up & Hooded Knitwear, this reinforcement is non-negotiable. By locking down these construction standards during initial development, we ensure that the sweater’s shoulder-to-hem ratio remains stable through heavy wear, preventing the fabric from collapsing under the weight of the metal teeth.
Which release checks should be agreed?
Validating full zip sweater quality requires rigorous, standardized physical testing during the pre-production and inline phases to catch dimensional and mechanical failures before the goods leave the factory. Relying solely on visual inspections will miss latent defects like poor zipper slider durability or chemical fiber degradation.
When should the buyer specify a zipper test?
The zipper assembly must withstand repeated mechanical stress throughout the lifecycle of the garment. We utilize physical testing equipment to verify the crosswise strength of the zipper chain and the pull-off strength of the slider. Partnering with certified third-party testing labs, such as the testing protocols outlined by Intertek Apparel Testing, allows us to perform objective assessments of seam strength and zipper durability under simulated consumer usage. Standard tests include 500 open-and-close cycles to guarantee that the zipper teeth do not separate or fail on retail floors.
How should dimensional change be recorded?
Beyond mechanical tests, we assess dimensional stability by subjecting finished sweaters to multiple wash cycles. We measure the change in length, width, and spirality (the twisting of the side seams). The order should state the measurement points, care cycle, accepted dimensional change, appearance standard, sample size, method, and disposition if the result fails. Add zipper colour transfer, pH, seam or slider tests only when they are relevant to the material, market and claimed performance, then obtain an order-scoped report. A standard or laboratory service describes a method or capability; it does not prove compliance for an untested order.
What needs to be fixed before bulk release?
Confirm the exact zipper and placket construction, retained PP sample, measurement record, care-cycle outcome, inspection plan, and change authorization before booking bulk. A source can inform the control: CottonWorks knit basics supports construction vocabulary, Woolmark care guidance frames fibre-care questions, ISO 2859-1 explains acceptance-sampling concepts, and Intertek apparel testing identifies available testing services. The order-specific record remains the evidence of the release.
Which published guides can support the buyer file?
Use tech-pack essentials, manufacturer evaluation, MOQ controls, low-MOQ checks, OEM and ODM selection, supplier comparison, bulk consistency, cable-knit development, and sourcing-model comparison.
Conclusion
Manufacturing a premium full zip sweater requires a deep technical understanding of the relationship between flexible knitwear and rigid zipper components. By establishing strict guidelines for zipper gauge matching, pattern symmetry, stabilized plackets, and wash-tested dimensional stability, brands can successfully mitigate the risk of buckling and distortion in bulk production. Partnering with a technically proficient manufacturer is the most effective way to transition your creative design concepts into retail-ready garments that maintain their fit over time. We invite you to explore our premium custom knitwear solutions on cnsweaters.com to discuss your upcoming collection. Please send your artwork, tech pack, garment type, quantity, fabric choice, target delivery date, and branding requirements to our development team for a comprehensive sample feasibility review, and let us help you build a reliable, high-performing knitwear line.
Frequently Asked Questions
What is the typical MOQ for custom full zip cardigans, and how does yarn choice affect it?
Our minimum order quantity (MOQ) for custom full zip knitwear is typically 300 pieces per style, which can be split across two colorways depending on the design complexity. This MOQ is directly dictated by the minimum spinning and dyeing volumes required by our yarn mills. For specialized fibers like custom merino wool blends, the MOQ may increase to 500 pieces because sourcing small dye lots of high-grade wool yarns is not economically feasible. If you choose to utilize our in-stock cotton or acrylic blend yarns, we can occasionally accommodate smaller test orders of 150 to 200 pieces, though this may incur a small-batch surcharge.
What are the typical sample lead times for a full zip knit sweater development cycle?
Sample timing should be a dated critical path, not a generic promise. Ask the supplier to list when yarn, zipper, custom hardware, artwork, sample assembly, testing, dispatch and approval become dependencies, and how a rejected item changes the plan.
How do you mitigate bulk production risks like zipper waviness before shipping?
We eliminate bulk manufacturing risks by running a rigorous “golden sample” protocol. Once the pre-production sample is approved, we lock in the knitting machine tension files, sewing thread density, and placket stabilization tape specifications. During bulk sewing, we perform hourly inline inspections, measuring the front placket length of assembled cardigans against the locked-in specification. Any panel showing deviation is immediately rejected. Additionally, we conduct random pull tests and laundry shrinkage verifications on 10% of every production batch to ensure no unapproved yarn variations have altered the dimensional stability of the finished goods.
How should brands plan their reorder timelines to avoid stockouts during peak seasons?
To ensure seamless inventory flow, brands should place their autumn and winter reorders at least 60 to 75 days in advance of their target delivery date. High-quality flatbed knitting machinery is heavily booked from May through October worldwide. A typical bulk production cycle takes 45 days, with an additional 15 to 30 days required for ocean freight shipping depending on your destination port. If you plan ahead, we can hold pre-allocated yarn reserves in our warehouse, reducing the production lead time for recurring styles to just 30 days, allowing you to react quickly to mid-season retail demand.